High-Calorific Refuse Derived Fuel (RDF) & Co-Processing
Supplying precision-shredded, low-chlorine alternative fuel fluff and dense briquettes with Gross Calorific Value (GCV) >3,800 to 4,200 kcal/kg, enabling 15% to 25% thermal coal replacement in heavy industry with zero bottom ash and statutory Category III CPCB destruction certificates.
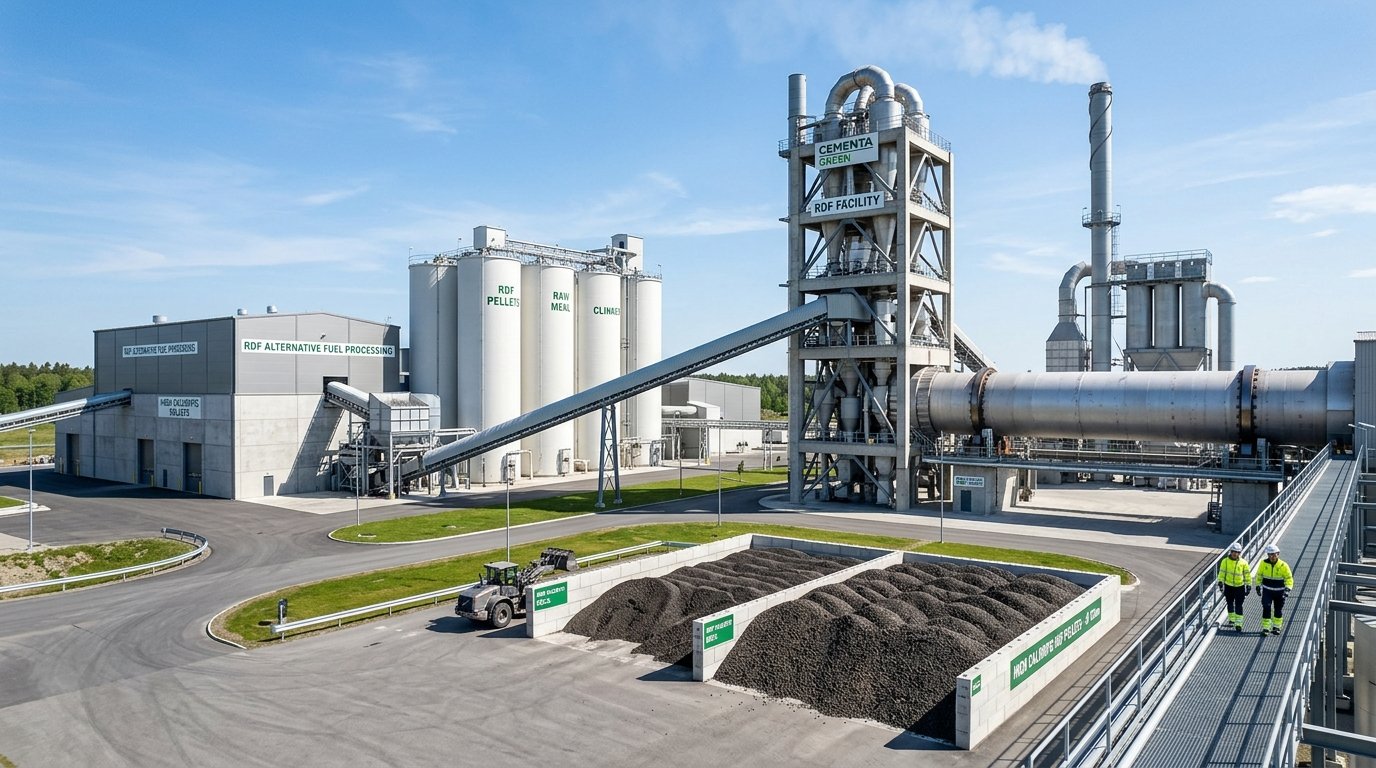
Engineered Quality for Industrial Kilns
Delivering stable pre-calciner operation without refractory corrosion or clinker contamination.
ASTM D5865 Certified Energy Density
Guaranteed Gross Calorific Value (GCV) exceeding 3,800-4,200 kcal/kg, delivering superior combustion performance compared to domestic grade coal.
Kiln Refractory Protection (Cl < 0.5%)
Dual-stage chemical and optical de-chlorination checks ensure chlorine levels remain strictly under 0.5%, safeguarding kiln refractory brick linings from acidic erosion.
Optimal Moisture Conditioning (< 12%)
Controlled thermal rotary conditioning keeps moisture under 12%, preventing flame quenching and maintaining stable pre-calciner temperatures.
Complete Clinker Mineral Absorption (Zero Bottom Ash)
Combustion residue is 100% incorporated into cement clinker minerals, resulting in zero secondary fly ash or bottom ash disposal issues.
RDF Processing & Co-Processing Lifecycle
From source sorting to direct pneumatic kiln injection with continuous laboratory validation.
High-Calorific Extraction
Automated sorting of combustible multilayer plastics, packaging films, and contaminated dry paper from municipal MRFs.
High EnergyMulti-Stage Shredding
High-torque primary and secondary shredding down to <30mm fluff, followed by ballistic air classification to remove inerts.
Uniform FluffThermal Drying & Testing
Rotary dryer moisture extraction below 12% and laboratory testing ensuring chloride concentrations remain below 0.5%.
Refractory SafeOff-Take & CPCB Credit
Enclosed bulk carrier transport to kiln pre-calciners with online CPCB destruction certificates issued for Category III obligations.
Zero AshWhat's Included in RDF Supply Contracts
Guaranteed bulk alternative fuel delivery with rigorous batch lab reports, CPCB Category III destruction credits, and kiln refractory warranties.
Request Industrial RDF Supply Contract
Inquire about annual bulk off-take contracts, thermal substitution rates, and sample laboratory testing parameters.
Frequently Asked Questions
Technical answers for cement manufacturing and boiler plant teams.
Our engineered industrial RDF meets ASTM D5865 standards with a guaranteed Gross Calorific Value (GCV) between 3,800 and 4,200 kcal/kg, moisture content strictly below 12%, and chlorine levels under 0.5% (Cl < 0.5%) to safeguard refractory linings in cement kilns. Every bulk dispatch includes batch laboratory testing reports.
RDF replaces 15% to 25% of costly imported fossil coal, significantly reducing operational fuel expenditures. Because plastic combustion ash is absorbed into cement clinker minerals, there is zero residual ash disposal. Environmentally, kilns achieve significant Scope 1 carbon emission reductions and earn alternative fuel thermal substitution credits.
Yes. Under CPCB PWM Rules, non-recyclable Category III plastic packaging can only be legally neutralized through certified thermal co-processing or waste-to-energy. Our co-processing contracts generate direct, audit-proof Category III disposal credits.